Capabilities
Tooling, molding and inspection in one Wenzhou factory — every critical step from drawing to mass production happens in-house, under our own roof.
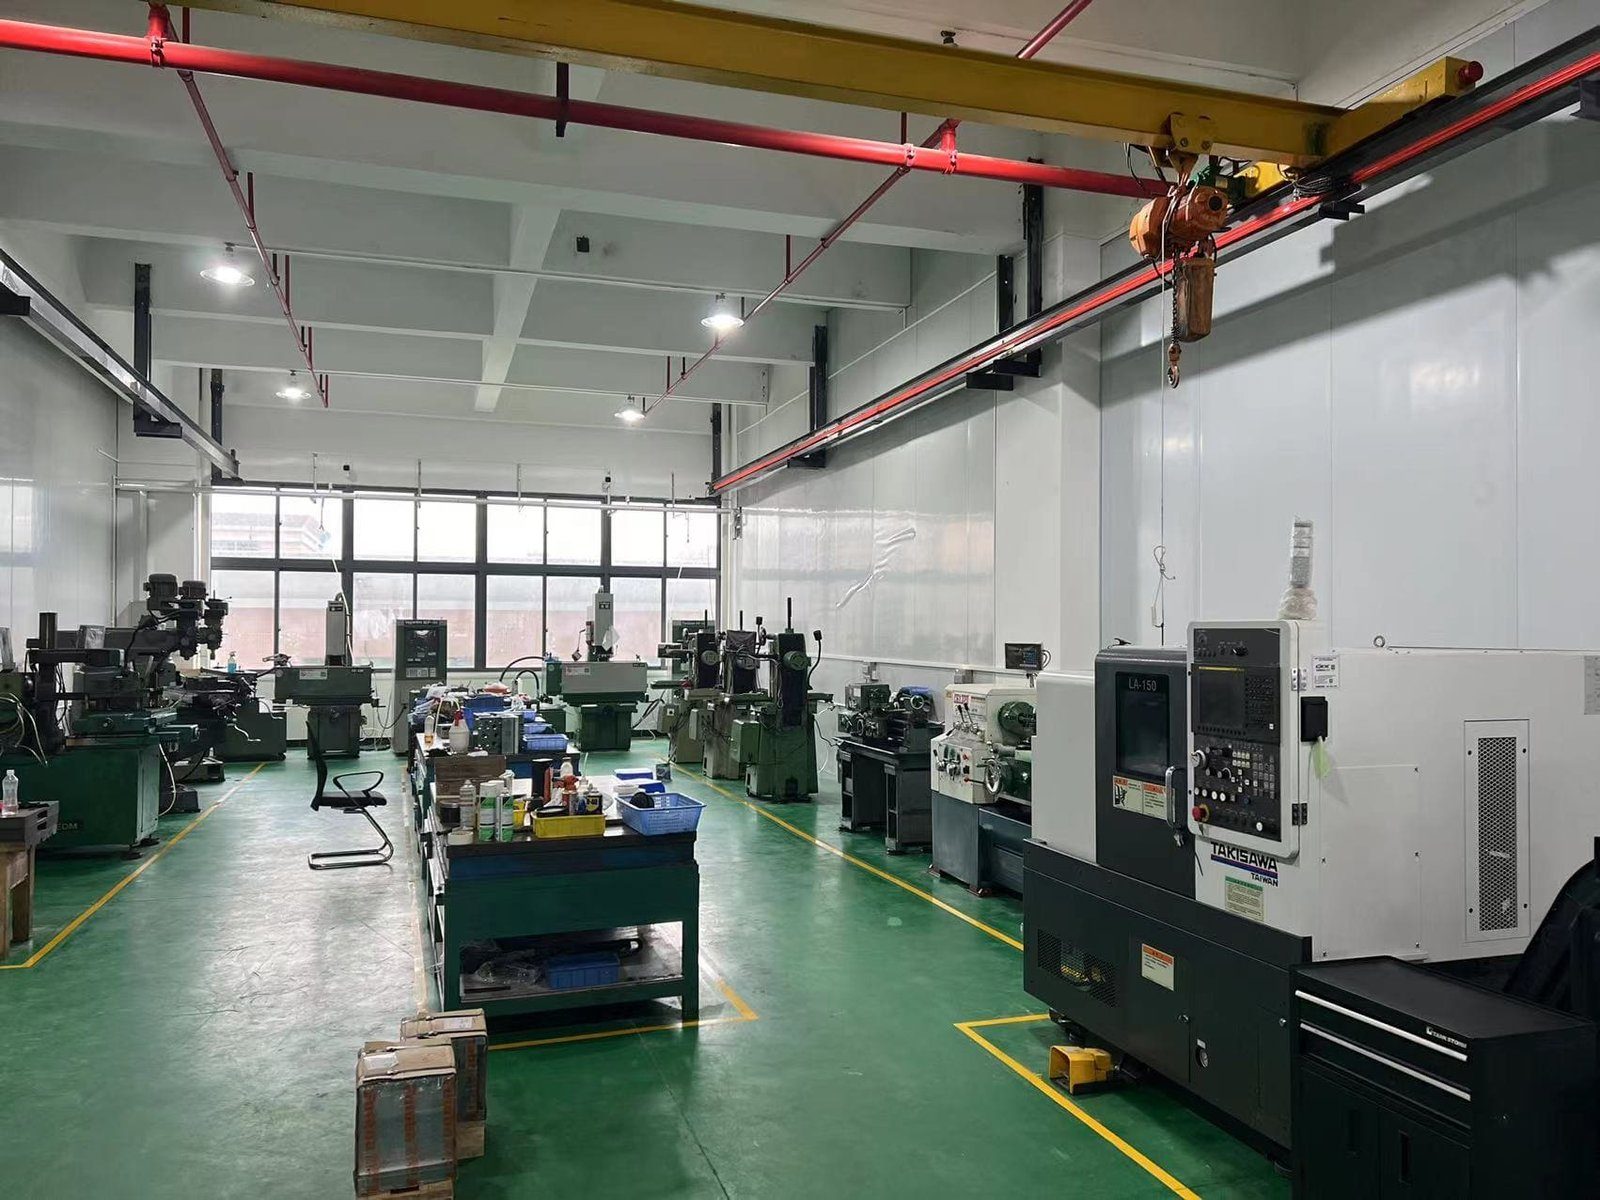
In-House Tooling
Tooling is where a plastic gear is won or lost: tooth profile accuracy is cut into the mold, not added later. Our molds are designed, machined, tried and maintained in our own tool room.
- Mold design & machining — gear cavities cut to your drawing, with shrinkage compensation for the chosen material.
- Mold trials in-house — first shots are molded and measured here, then the tool is corrected.
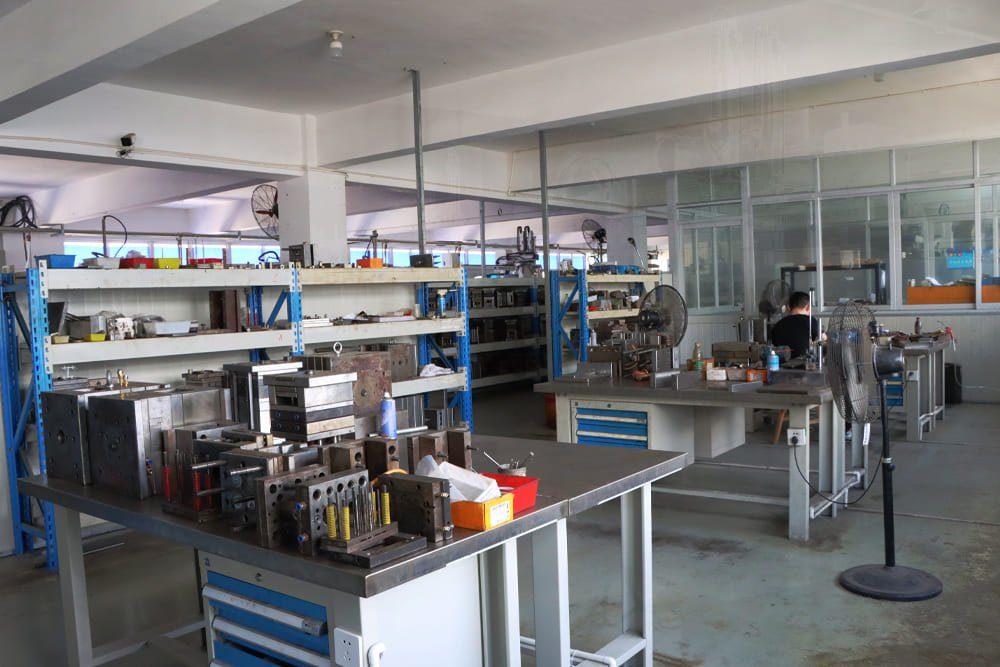
- Repair & maintenance — when a mold needs work mid-project, our own tool room handles it; production is not waiting on an outside shop.
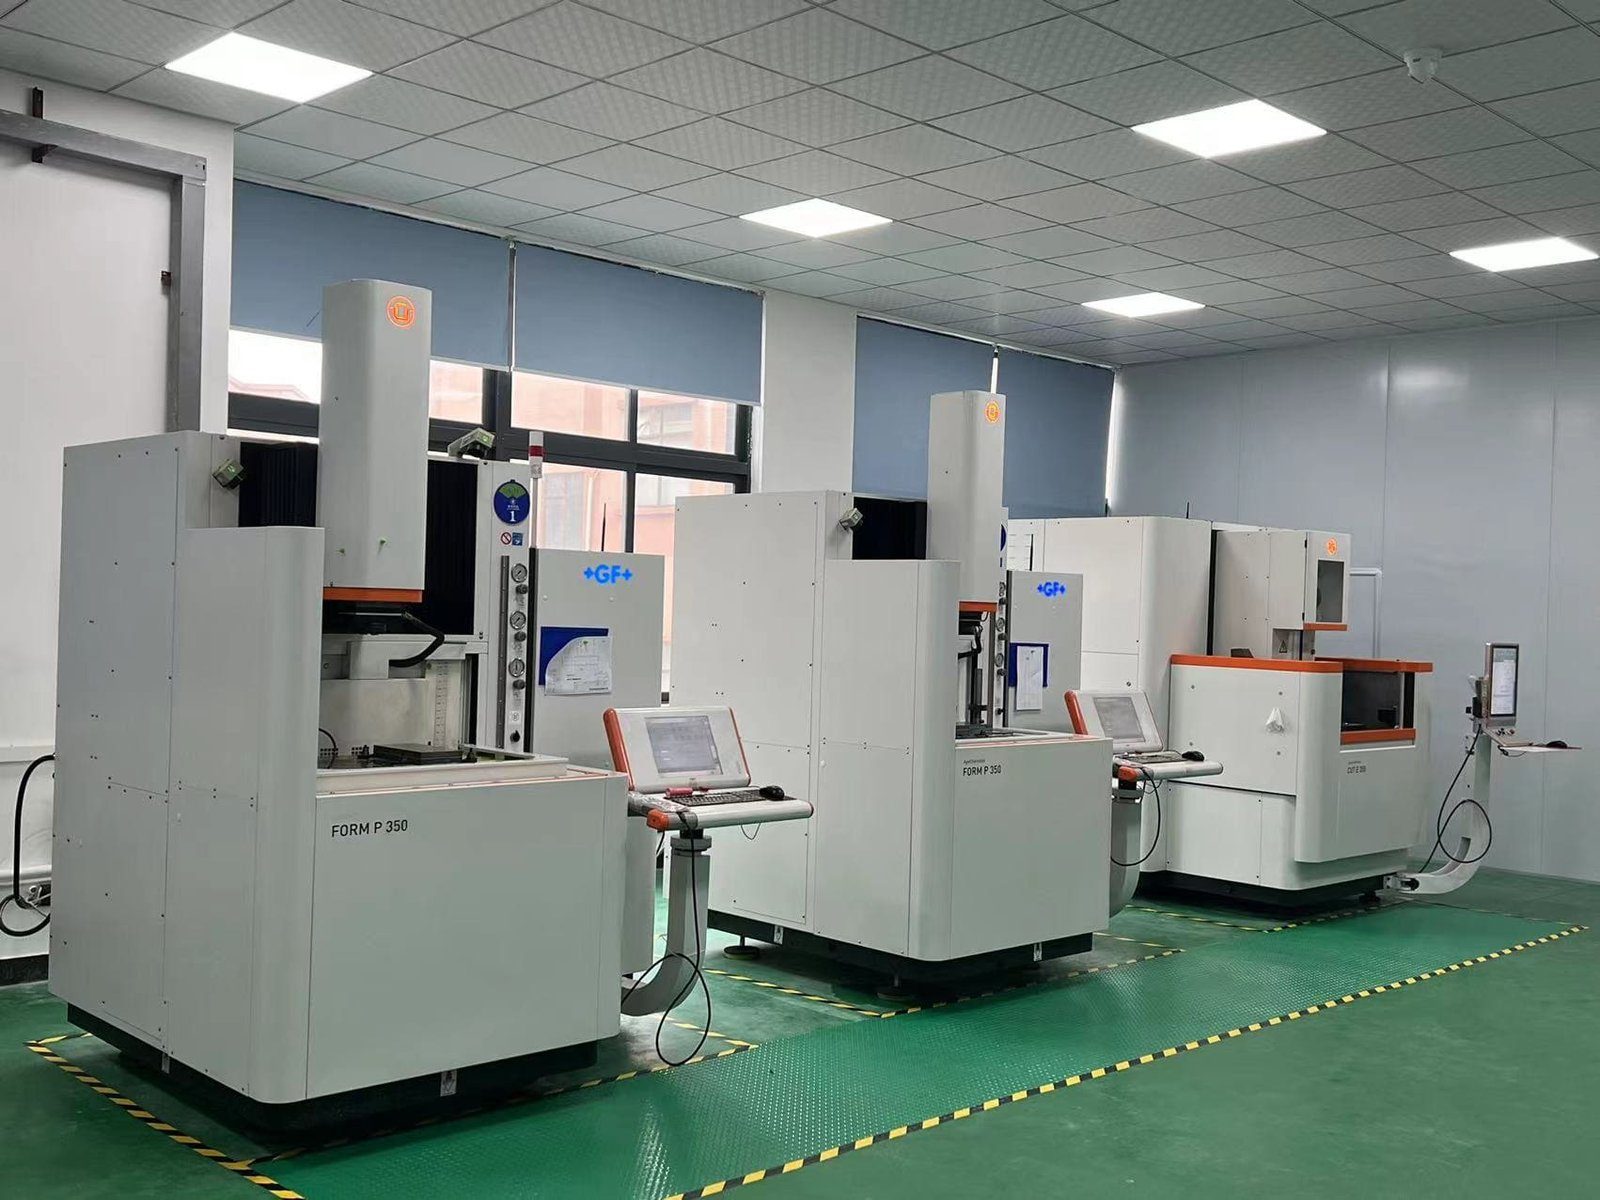
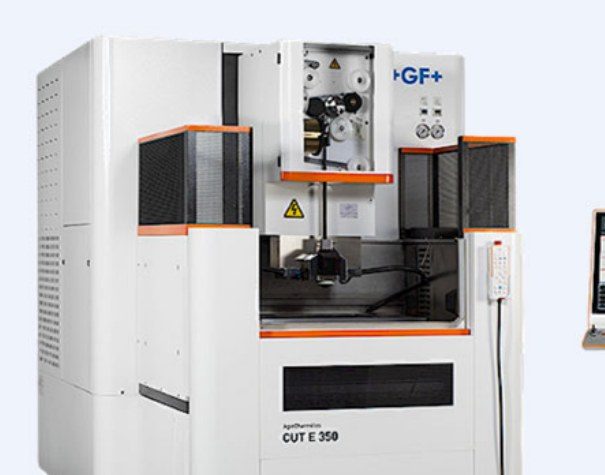
- Slow-wire EDM and precision electrodes for micro gear cavities down to module M0.1
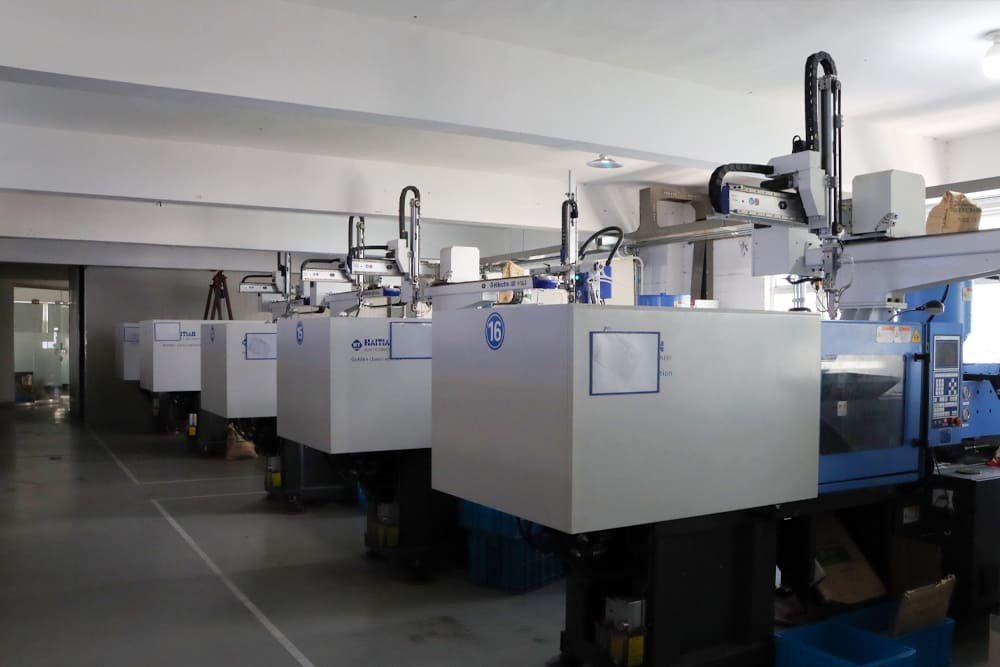
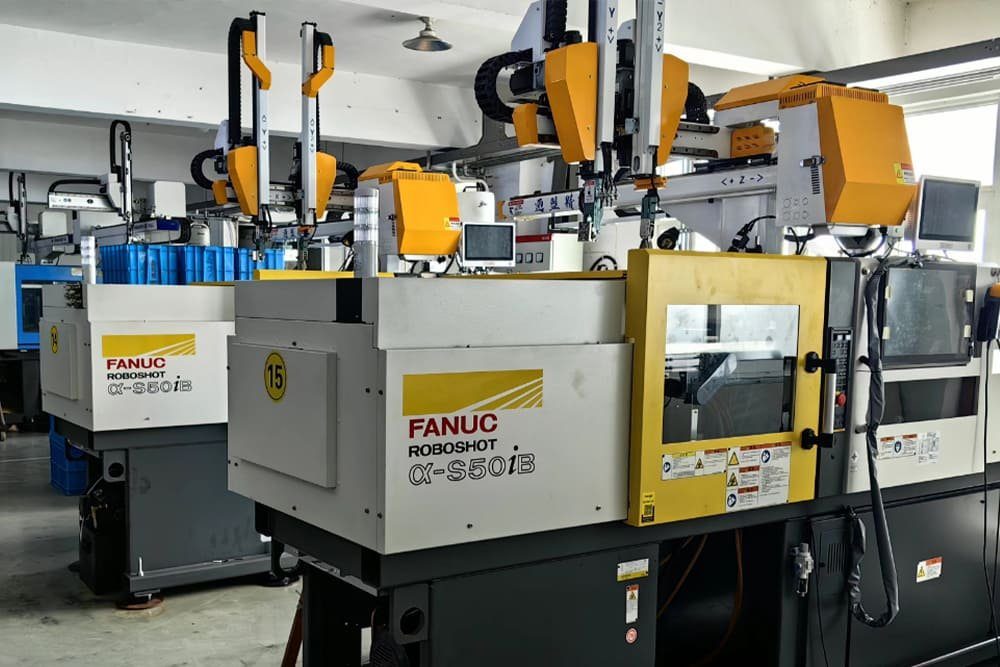
- Molding capacity of around 24 machines from 35 to 160 t — Nissei, FANUC ROBOSHOT α-S50iB, Arburg and Donghua — covering micro parts through to larger housings, including insert and overmolding work
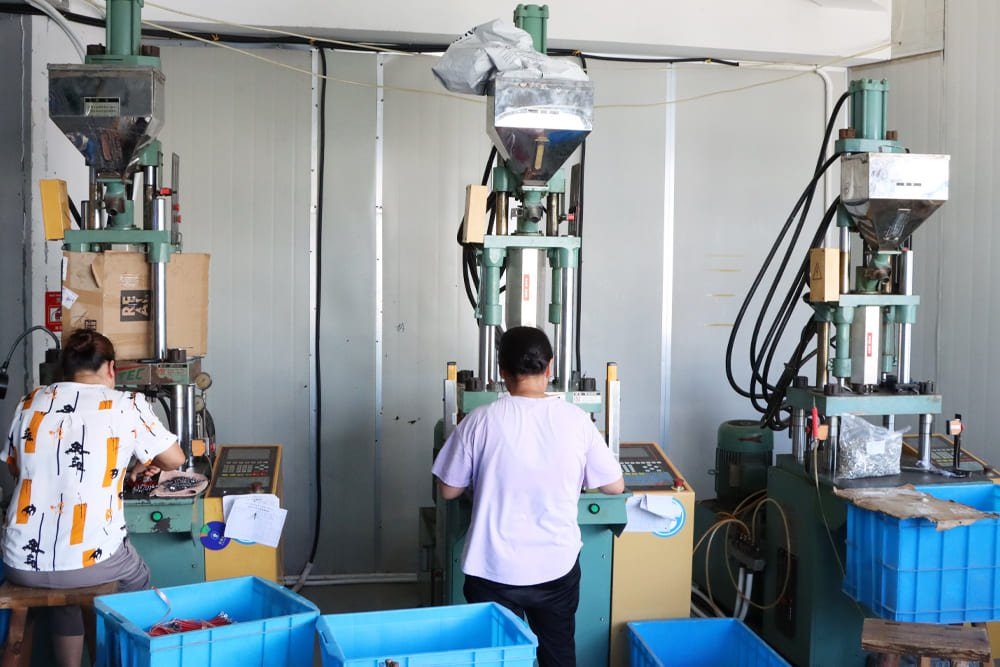
Injection Molding
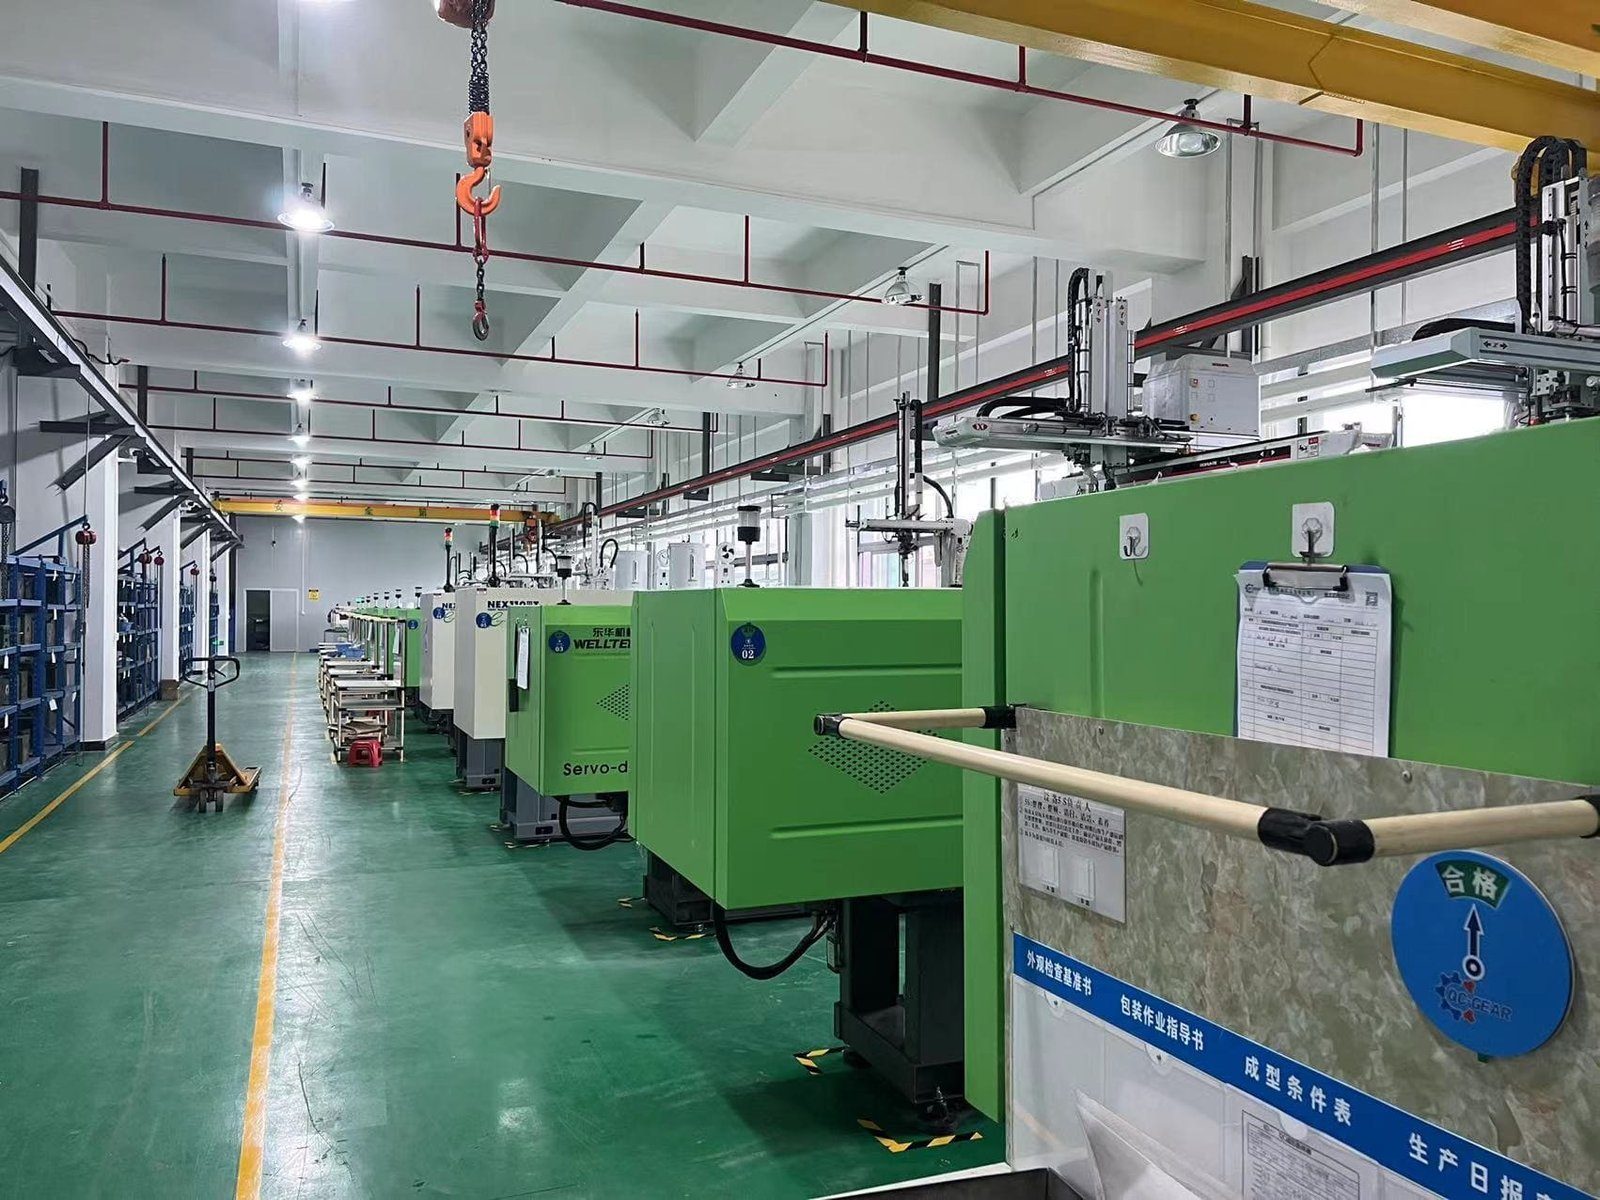
Gears are molded on Japanese all-electric injection molding machines, including FANUC ROBOSHOT. All-electric drive gives stable, repeatable cycles — what small-module gear teeth need, shot after shot.
- Gearboxes assembled with their molded housings in the same factory.
- Materials processed daily: POM, Nylon, PC and ABS.
Transmission Design & Engineering
For micro and small drives, engineering can start before your drawing is final. Support covers the whole transmission, not just the molding: High-precision custom work is a core strength: precision molds and high-precision gears are designed and made to your drawing, not adapted from stock parts.
- Meshing analysis and gear geometry design
- Tooth profile modification (tip and root relief)
- Tooth root strength and contact stress analysis
- Transmission simulation and mold-flow analysis
- Precision gear mold inserts and copper electrodes machined in-house — GF AgieCharmilles slow-wire EDM (E350) and die-sinking EDM (P350) for micro cavities
Gear Types We Mold
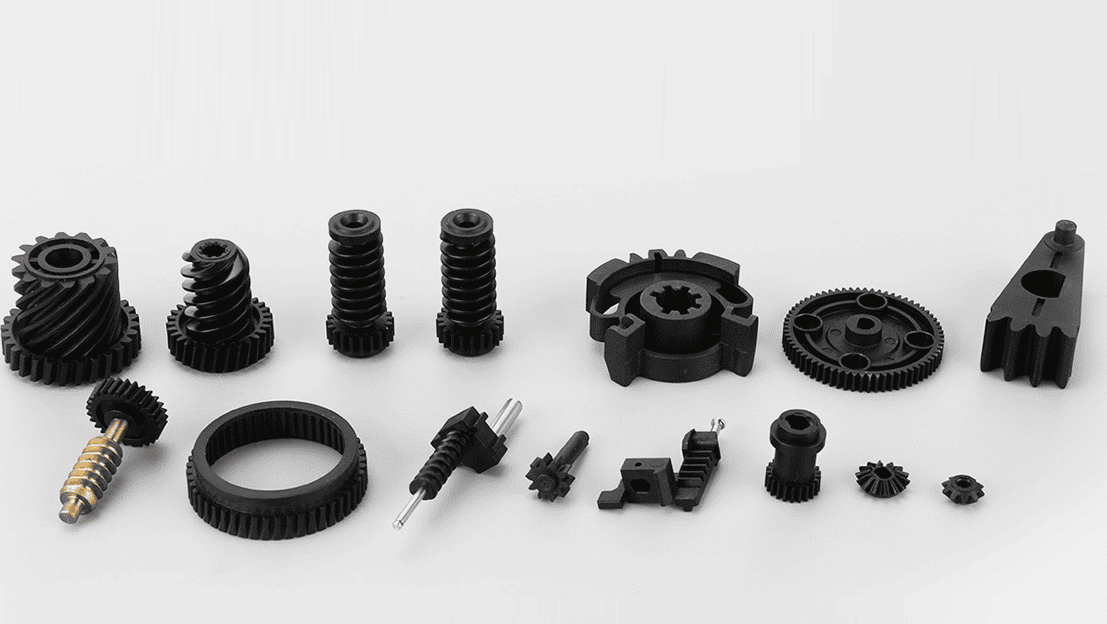
Seven gear forms cover nearly every small drive used in actuators, appliances and devices.
Materials
Four engineering plastics cover most gear and housing jobs. We will recommend a grade after reviewing your drawing and load case.
POM
Polyoxymethylene · Acetal
The workhorse gear material: stiff, low-friction and dimensionally stable, with crisp tooth definition straight from the mold.
Nylon
Polyamide · PA
Tough and wear-resistant, with good impact strength — a common choice for higher-load gears and worm wheels.
PC
Polycarbonate
High impact strength and heat resistance; used for demanding components and parts where toughness matters most.
ABS
Acrylonitrile Butadiene Styrene
Easy to mold, economical and rigid — the standard choice for gearbox housings and covers.
From Drawing to Production
Eight steps, each with its own quality gate — from drawing review with DFM to a final re-inspection before shipment.
Drawing Review & DFM
We check tooth geometry, tolerances and moldability, and send DFM feedback before quoting tooling.
Transmission Design Confirmed
Gear geometry, ratio and materials are confirmed with you — with meshing analysis and mold-flow checks where the drive needs them.
Mold Making
The mold is designed and machined in our own tool room, its cavities cut to your drawing.
T1 Samples
First shots off the new mold (T1) are molded and prepared for measurement.
Sample Inspection Report
Samples are measured — double-flank meshing and key dimensions — and the report goes to you with the samples.
Your Approval
Production starts only after you approve the samples and the report.
Mass Production
Approved parts run on our injection machines, with checks at set intervals during the run.
Final Inspection & Shipment
Finished parts are re-inspected before packing — what ships is what you approved.
Quality Inspection
Inspection is built into the process, at four points:
Incoming Materials
Resin is checked on arrival before it is released to production.
First-Article Inspection
First parts off a new or corrected mold are measured against the drawing before production is approved.
In-Process Checks
Parts are checked at intervals during the production run, not just at the end.
Final Inspection
Finished parts are inspected before packing and shipment.
Inspection reports and material certificates are available on request — tell us what documentation your incoming QC needs when you enquire.
Gear Measurement & Drive Testing
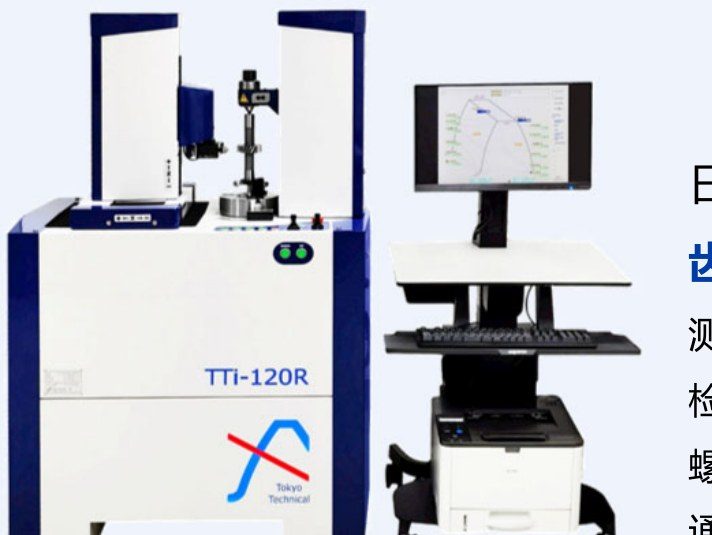
Gear trains and complete gearboxes are also tested as drives — measurement, noise, torque and endurance:
Measured Precision — Sample Test Report
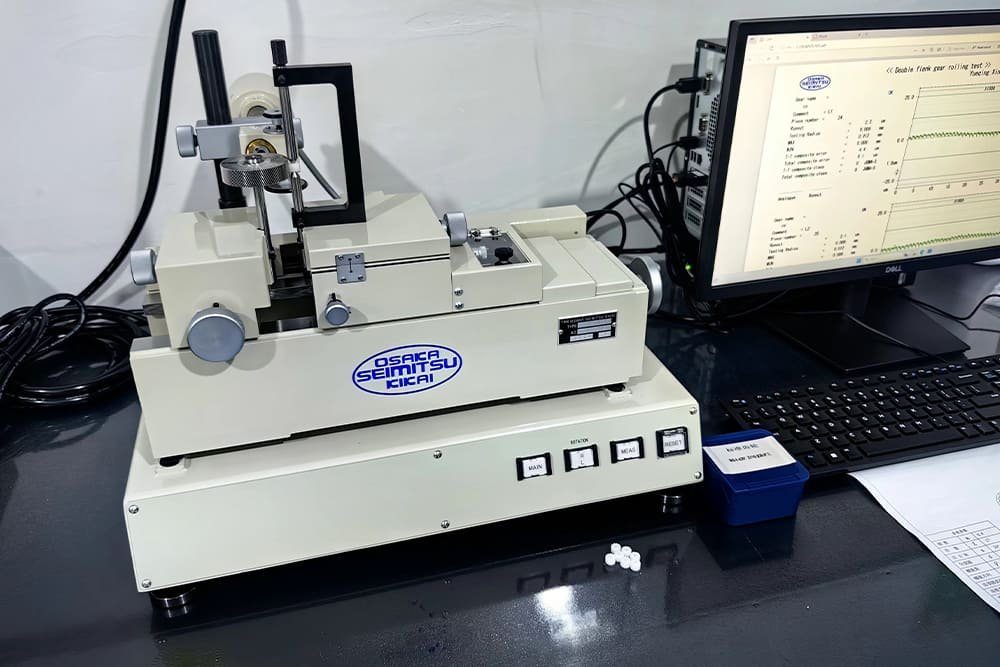
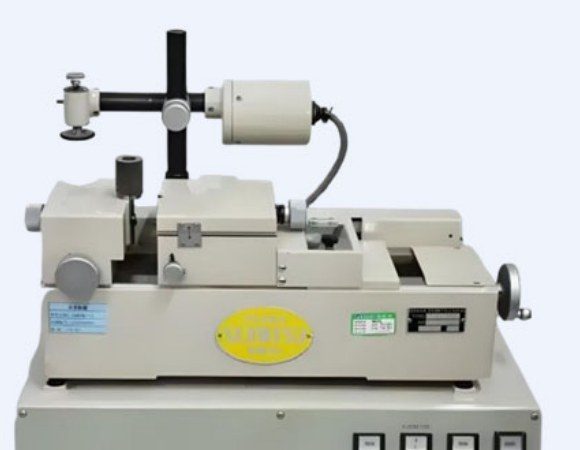
One sample gear from our production, measured on our Osaka Seimitsu double-flank (double-sided meshing) tester. The sample: module 0.320, 9 teeth.
- Gear accuracy
- JGMA Grade 0 — measured on the sample
- Tooth-to-tooth composite error
- 2.8 µm
- Total composite error
- 4.1 µm
- Runout
- 1.4 µm
This is a sample measurement report: it documents the precision level our tooling and molding reach on micro gears. It is not a blanket guarantee for every part — your parts are measured against your drawing and its tolerances.
Factory Tour
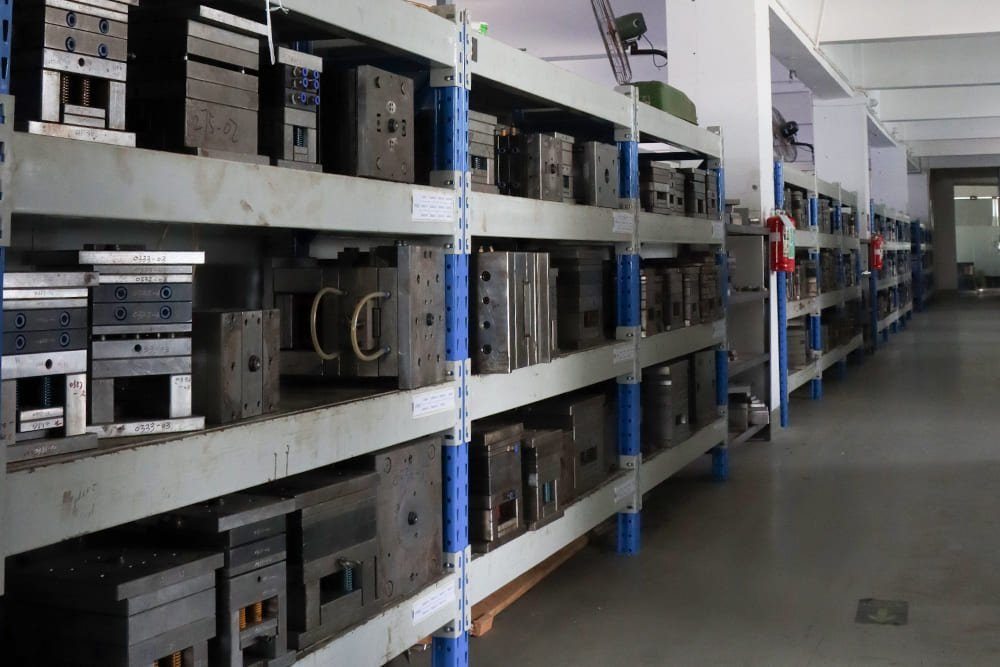
The rest of the floor, as it is — molding, tooling, mold storage and the benches where molds are assembled and maintained.
Put our tool room to work
Send a drawing and we will tell you honestly whether we can mold it — and what it will cost.